Surface Finishing for Polymer and Plastics Production Equipment
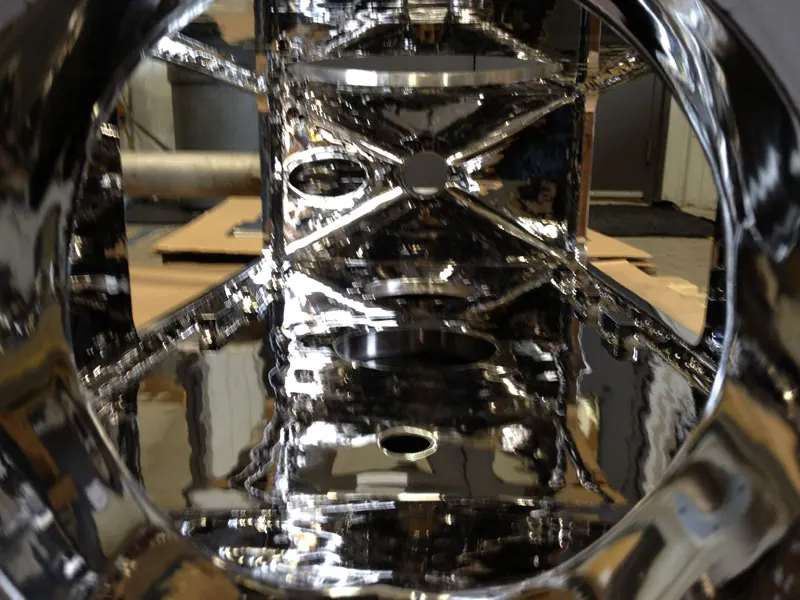
The short answer: Product buildup is the hidden cost in a polymer plant. Pellets, powders and melt cling to the microscopic peaks on as-fabricated stainless, transfer rates fall, stringers and angel hair form, and the line shuts down to clean. Harrison polishes the product-contact surfaces — hoppers, conveyor screws, rotary valves, transfer lines, dies and vessel interiors — so product releases instead of building up. Intervals between cleaning shutdowns get longer and the cleaning itself gets shorter.
Equipment we finish
Hoppers, silos and bins. Interior polishing to keep pellets and powders flowing and reduce bridging.
Conveyor screws and rotary valves. Electropolished or mechanically polished flights, housings and rotors; see reducing product adhesion.
Transfer lines, elbows and diverter valves. Interior polishing to reduce stringers and angel hair at bends.
Dies, mixers and vessel interiors. Mechanical polishing, electropolishing or the Harrison C-75 process depending on material and finish target.
Choosing the process
Electropolishing dissolves the microscopic peaks and leaves a featureless, chromium-rich surface with the lowest adhesion and best corrosion resistance; it is the usual choice for stainless product-contact surfaces. Mechanical polishing reaches a specified Ra on surfaces or materials electropolishing cannot, and is the first step before electropolishing when the starting surface is rough. The Harrison C-75 process is our polishing process developed for product-release surfaces in bulk-solids handling. We recommend based on your material, the equipment geometry and the finish specification rather than defaulting to one process.
Capacity and turnaround
The Houston facility has four overhead cranes and 15,000 lb material-handling capacity for large hoppers and screw assemblies, and Harrison field crews polish and passivate installed equipment throughout the Houston area and the Gulf Coast. We have served polymer and petrochemical producers since 1980 and are ISO 9001 and ISO 14001 certified. Expedited service is available for shutdown windows; lead times vary with shop load.
Representative project
A Gulf Coast polymer producer was losing throughput to pellet buildup and stringers in a set of stainless transfer lines and the rotary valves feeding its extruders. Harrison electropolished the line interiors and elbows, polished the rotary-valve rotors and housings, and returned the equipment inside the planned shutdown with certificates of conformance. Buildup in the lines dropped, stringer formation at the elbows fell, and the producer extended the interval between cleaning shutdowns.
Request a polymer equipment quote
Tell us the equipment, the material, the product that is building up, and your shutdown dates. We quote within one business day.
Request a Quote · Call 800-245-5707
- More to Know
Frequently Asked Questions
Services
Resources
13002 Brittmoore Park Dr
Houston, TX 77041-7231
Phone: 800-245-5707